
Hydraulic valves for tunnel construction machinery must withstand continuous dust, pressurized water, mechanical vibration, and unstable generator power — conditions that cause standard industrial valves to fail within 200–400 hours. Key requirements include IP67-rated connectors, 28V wide-range solenoid coils, and modular directional valve banks rated for 210–315 Bar.
Tunnel construction machinery operates in one of the most extreme hydraulic environments on earth — continuous dust, pressurized water ingress, generator-sourced power fluctuations, and high-frequency drilling cycles.
Standard industrial hydraulic valves are not built for these conditions. The result is coil burnout, connector failure, and directional valve seizure — typically within 200–400 operating hours.
This guide covers:
- Why standard valves fail underground
- Which hydraulic components arch-anchor machines require
- How to specify valves for tunnel OEM applications
- A field-verified case from Rekith Hydraulics
Types of Hydraulic Valves Used in Tunnel Construction Equipment
Tunnel construction machines rely on three functional valve categories, each with a distinct role:
| Ventil Typ | Funktion | Tunnel Application |
|---|---|---|
| Richtungsabhängige Steuerventile | Route fluid to actuators, control movement direction | Boom steering, arch positioning, drill feed/retract |
| Druckregelventile | Limit and regulate system pressure | Circuit protection, sequence control, load holding |
| Durchflussregelventile | Regulate actuator speed | Drilling feed rate, grouting pump output control |
For arch-anchor integrated machines and jumbo drill rigs, directional control valves — especially multi-section modular banks — are the highest-criticality components due to the number of simultaneously controlled actuators.
What Causes Hydraulic Valve Failure in Tunnel Construction Equipment?
Hydraulic valves fail in tunnel construction equipment due to three root causes:
- Dust and water ingress — rock dust and water spray penetrate standard connectors, causing coil short circuits
- Vibration-induced wear — 20–80 Hz drilling vibration loosens connectors and erodes spool surfaces
- Generator power fluctuation — ±15% voltage variation overheats coils wound for fixed 24V input
Each failure mode requires a specific engineering countermeasure, detailed below.
Why Standard Hydraulic Valves Fail in Underground Equipment
1. Dust and Water Ingress
Standard DIN solenoid connectors are rated IP54 at best. Inside an active tunnel, fine rock dust and pressurized water spray penetrate unsealed connector cavities within hours — causing insulation breakdown and coil short circuits.
Minimum IP requirement for tunnel applications: IP67 per IEC 60529.
2. Vibration-Induced Connector and Spool Wear
Percussive drilling and boom movement generate 20–80 Hz continuous vibration.
This causes:
- Connector loosening → intermittent electrical contact
- Spool surface wear → internal leakage and loss of holding stability
3. Coil Burnout from Generator Power Fluctuation
Remote tunnel sites run on diesel generators with ±15% voltage regulation.
A standard 24V coil operating at 27–28V continuously exceeds thermal limits.
Correct specification: 28V DC wide-range coil.
Key Hydraulic Components for Arch-Anchor Integrated Machines
The arch-anchor integrated machine combines arch frame installation, positioning, anchor drilling, and grouting in a single platform.
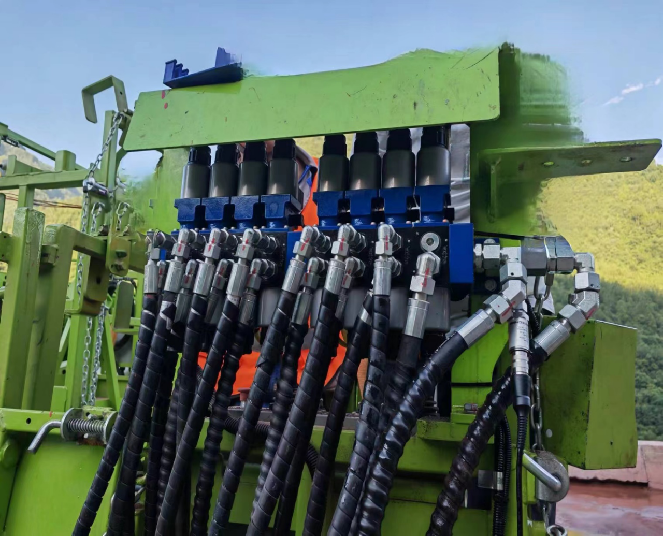
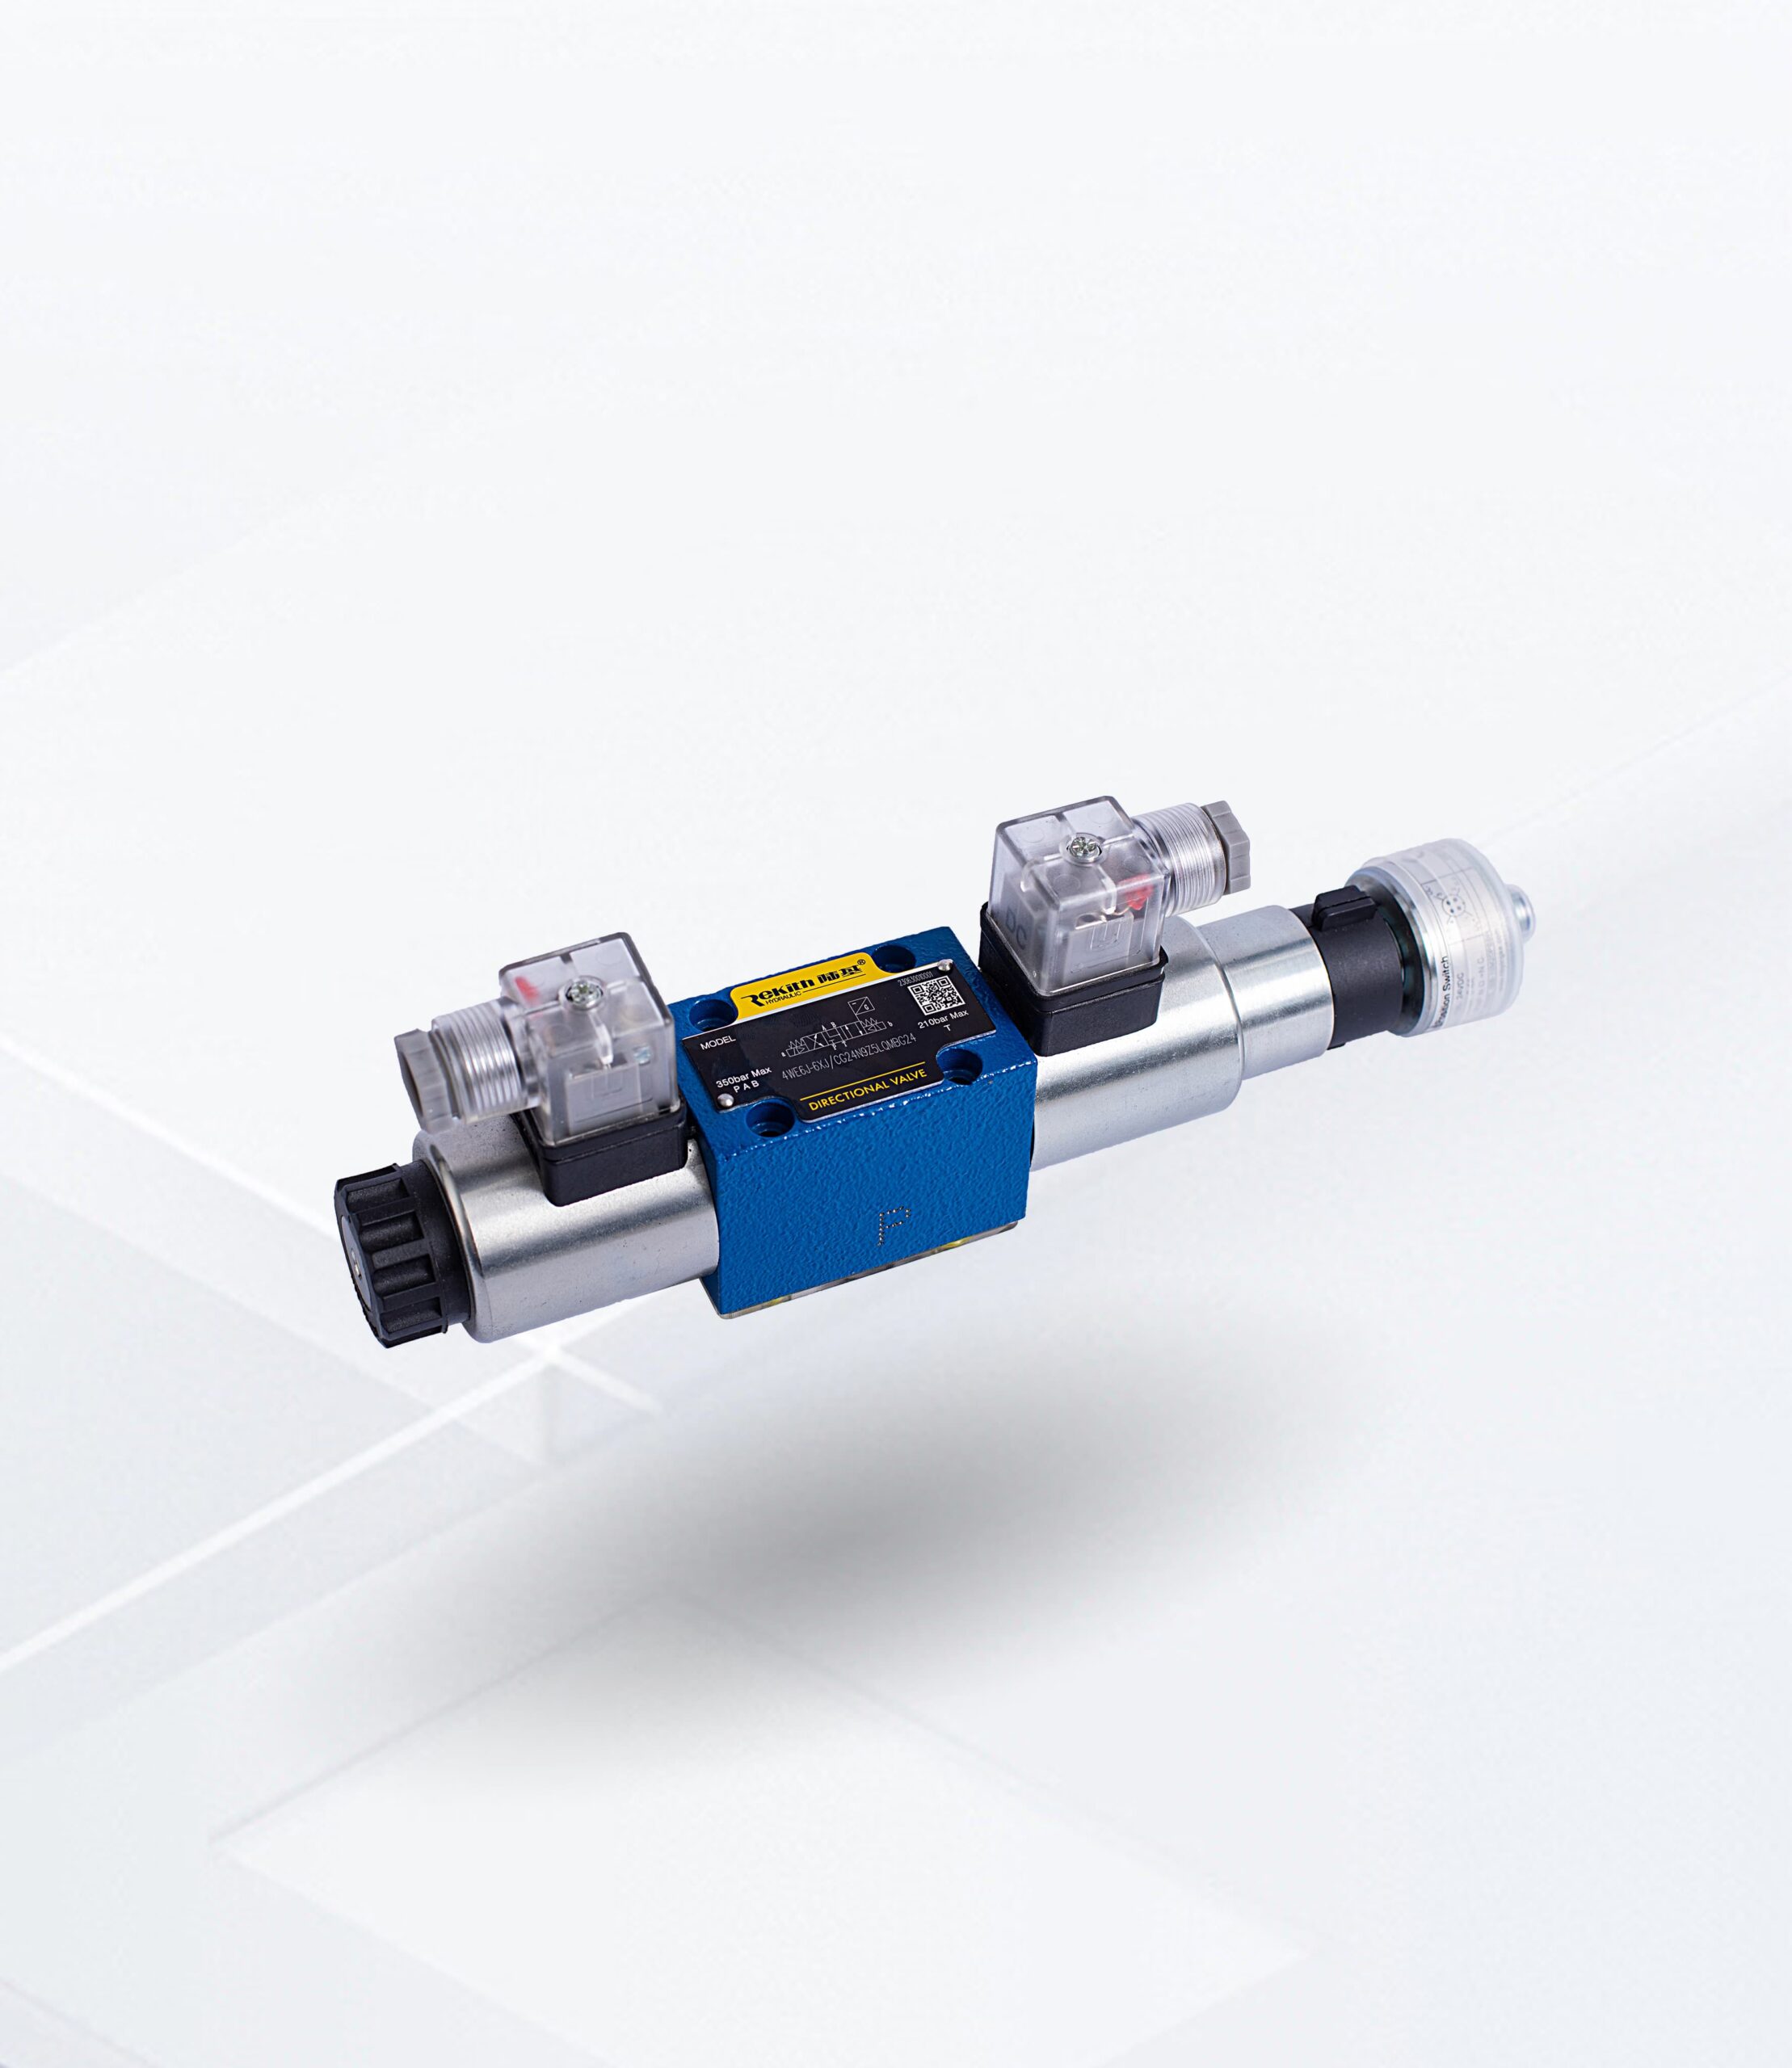
Modular Multi-Section Directional Valve Bank
| Spezifikation | Recommended Value |
| Sections | 6–10 (scalable) |
| Maximaler Betriebsdruck | 315 Bar |
| Steuerungsart | Solenoid direct-push |
| Expandability | Add/remove sections |
28V Wide-Range Solenoid Coil with Deutsch IP67 Connector
| Merkmal | Spezifikation |
| Spulenspannung | 28V DC wide-range |
| Connector Type | Deutsch DT series |
| Ingress Protection | IP67 |
| Encapsulation | Full-iron |
Rekith Application Case: Arch-Anchor Machine Valve Supply
Equipment Overview
| Parameter | Detail |
|---|---|
| Equipment Type | Arch-anchor integrated machine (tunnel initial support) |
| Actuator Count | 8 independent arms |
| Operating Altitude | Up to 4,500m ASL |
| Umwelt | Active tunnel face — dust, water spray, vibration |
Client Requirements
| Requirement | Detail |
|---|---|
| Valve Sections | 8 independently controlled directional valve sections |
| Coil Specification | 28V DC wide-range coil (diesel generator power supply) |
| Connector Type | Deutsch IP67 connector (tunnel washdown environment) |
| Gestaltung | Modular design scalable from 6–10 sections across model range |
| Muster-Vorlaufzeit | 5 days |
Rekith’s Delivered Solution
| Parameter | Delivered Specification |
|---|---|
| Ventil Typ | WE-series modular directional valve bank |
| Sections | 8 (scalable 1–12) |
| Working Pressure | 315 Bar |
| Spulenspannung | 28V DC wide-range |
| Connector | Deutsch DT series, IP67 |
| Seal Material | Viton |
| Muster-Vorlaufzeit | 5 business days |
| Batch Lead Time | 10–15 business days |
How to Select Hydraulic Valves for Tunnel OEM Equipment

Step 1 — Define Working Pressure and Flow Rate
Most tunnel hydraulic circuits operate at 210–315 Bar.
Select valves rated at minimum 1.25× system relief valve setting to ensure stability under shock load and peak pressure spikes.
Step 2 — Match IP Rating to Site Conditions
| Site Condition | Required IP Rating |
|---|---|
| Active tunnel face (drilling, water spray) | IP67 minimum |
| Covered equipment area | IP54 acceptable |
| Outdoor / exposed position | IP65 minimum |
Step 3 — Select Coil Voltage by Power Source
| Power Source | Coil Specification |
|---|---|
| Diesel generator (unstable site power) | 28V DC wide-range coil |
| Machine battery / alternator | 24V DC standard |
| Shore power with rectifier | 24V AC / 110–220V options |
Step 4 — Determine Section Count by Actuator
Count all independently controlled hydraulic functions.
Best practice:
👉 Actuator count + 1 spare section
This allows future expansion without redesigning the valve bank or manifold system.
Häufig gestellte Fragen
What IP rating is required for tunnel construction hydraulic valves?
For active tunnel environments, IP67 is the minimum standard. This ensures protection against both dust ingress and water exposure from drilling and washdown conditions.
Can these valves operate at high altitude?
Yes. Rekith valves are validated for operation up to 4,500 meters above sea level. We confirm coil performance and thermal limits based on your specified altitude.
What is the minimum order quantity?
You can start from 1 piece for samples. This allows you to test performance before committing to batch production.
Are these valves compatible with existing systems?
Many Rekith valves follow CETOP / ISO 4401 standards, making them compatible with common subplates and systems. Custom adaptations are also available based on your drawings.